Custom aluminium extrusion
Send a cross-section DXF or STEP and we'll quote the die, the per-metre price and any machining or anodising you need. We review wall balance, tongue ratios and shrink before the die is cut.
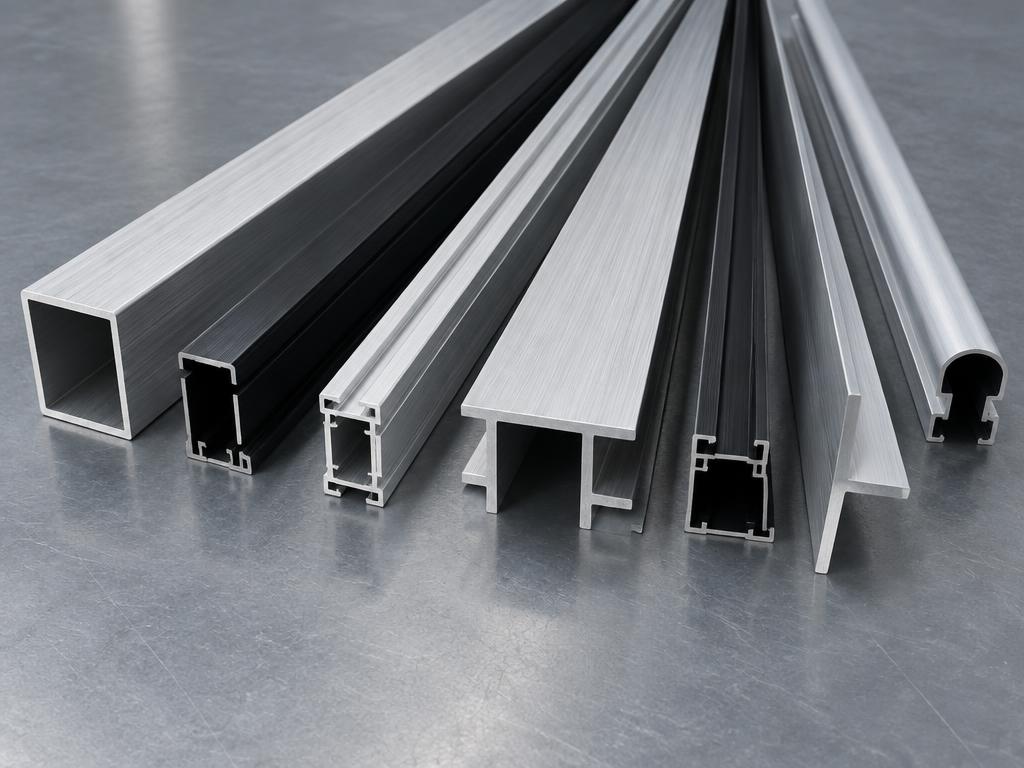
6060, 6063, 6082 in T5 and T6 temper
Up to 250 mm circumscribing circle, 0.8 mm minimum wall
Solid, semi-hollow and hollow dies, typically 2–3 weeks
Cut to length, CNC machining, tapping, punching, deburring
Mill finish, clear/black anodise, powder coat, brushed
150 kg per profile per order
Choosing a material
Select the alloy and temper together: an easy-to-extrude profile is not always the strongest. Include your required finish, visible surfaces and any load-bearing features in the enquiry.
- 6060
- Good formability for detailed profiles. Consider for decorative and general profiles.
- 6063
- Good surface finish and anodising response. A common choice for architectural enclosures.
- 6082
- Higher structural strength, with more geometry constraints. Consider for loaded frames and rails.
Planning an extrusion
Send the cross-section
A dimensioned DXF or STEP profile shows wall thickness, hollow features and the surfaces that matter. Include your cut length and order volume.
Review the die
Thin walls, uneven sections and deep slots can affect die design and straightness. We review the profile with a qualified extrusion partner before tooling.
Specify secondary work
Tell us about cut lengths, tapping, machining, anodising and cosmetic faces so the finished-part cost is included in the quote.
Related processes
If your part is not a continuous profile, one of these processes may be a better fit.
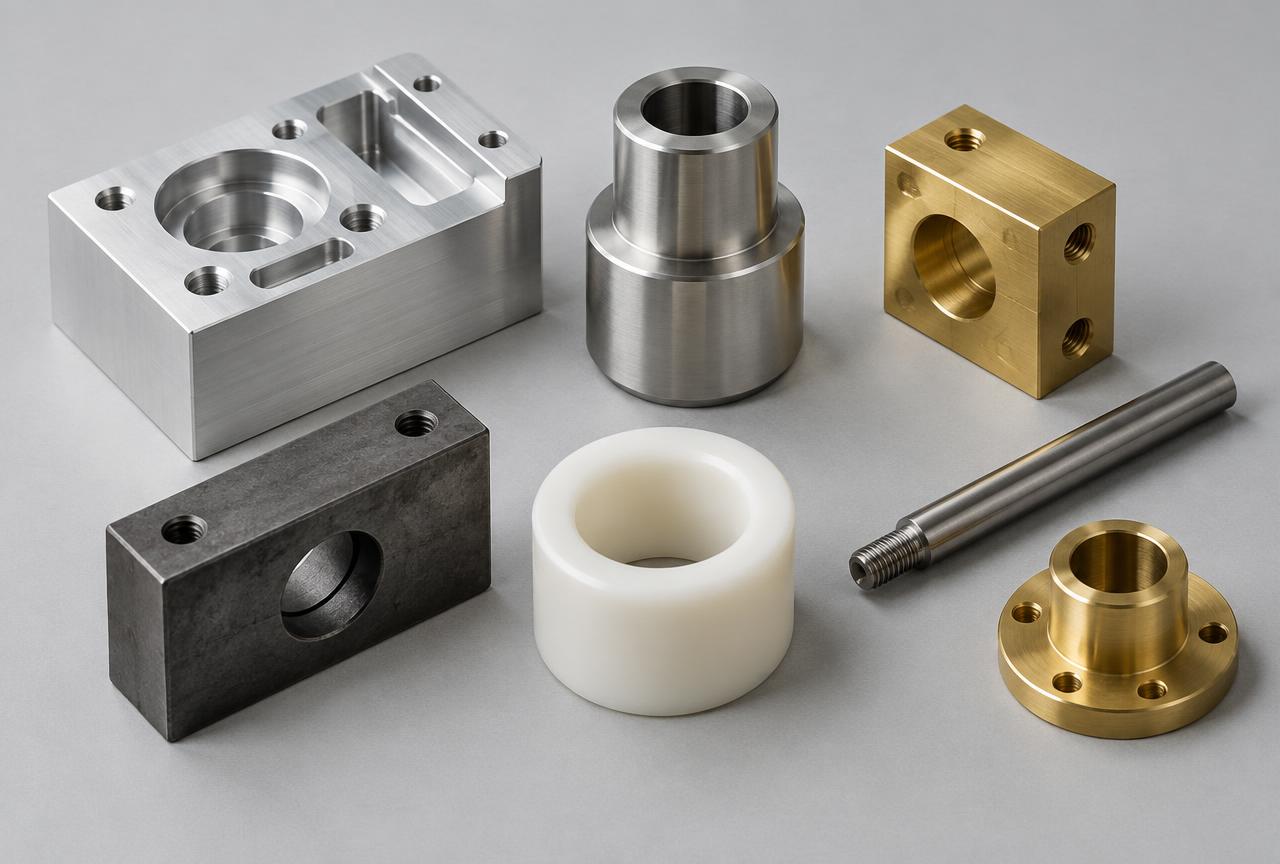
CNC machining
Better for low quantities, solid parts, or profiles that need extensive machining without extrusion tooling.
View serviceDie casting
Better for high-volume three-dimensional metal parts that cannot be produced as a constant profile.
View serviceSheet metal
Better for folded panels, brackets, and enclosures made from flat sheet at lower tooling cost.
View service